>>
Industry>>
Automotive>>
A Complete Practical Guide to ...A Complete Practical Guide to Plastic Injection Molding Basics
The Silicon Review
28 September, 2026
Author:
Guest
Plastic injection molding turns heated polymer into repeatable parts through pressure, cooling, and controlled tooling. The process suits components that require consistent dimensions, clean surfaces, and production at scale. Good results depend on more than selecting a resin and ordering a mold. Each stage of the process plays a role in the quality of the finished part.
Part geometry, material behavior, machine settings, and inspection criteria must work together. A detailed guide to plastic injection molding connects each production stage, helping designers make the right decisions before manufacturing begins. That foundation starts with a clear picture of how molten material becomes a finished component.
How the Process Works
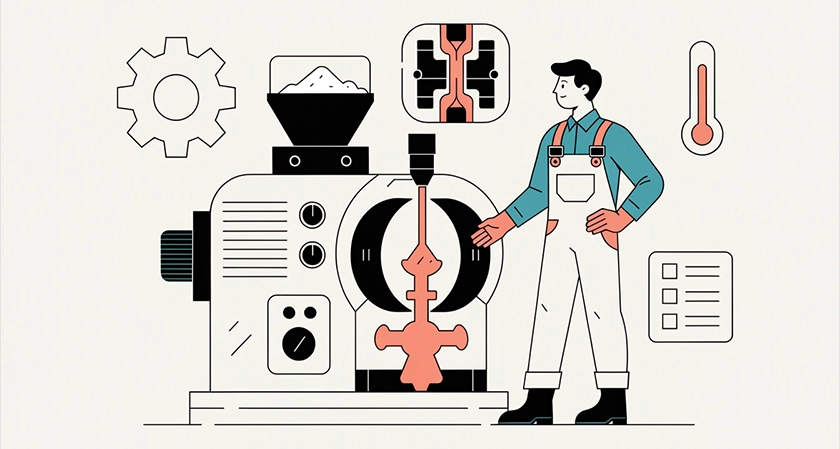
Plastic pellets enter a heated barrel, where rotating screws melt and mix the material. The screw then pushes the melt through a nozzle into a closed mold. Pressure fills the cavity, while cooling channels remove heat and allow the part to solidify. Ejector pins release the finished component after the mold opens. Understanding how these stages connect helps designers assess tooling, material selection, cycle timing, and quality requirements before production begins.
The cycle repeats after the mold closes again. Injection speed, holding pressure, cooling time, and barrel temperature affect dimensions, surface finish, and internal stress. A small change in one setting often changes the result because each stage affects the next.
Designing the Part for Molding
Part geometry determines how easily molten material fills the cavity and how cleanly the part leaves the mold. Uniform wall thickness reduces uneven cooling, sink marks, and warpage. Sudden thickness changes require gradual transitions or carefully placed design features.
Draft angles help molded surfaces release without scuffing or deformation. Ribs add stiffness with less material, but they should remain thinner than nearby walls to reduce sink marks. Bosses need support ribs and suitable openings when screws or inserts will be used.
Sharp internal corners create stress and restrict material flow. Radii at corners improve flow and reduce stress concentration. Designers should also identify parting lines, ejection points, gates, and visible surfaces before mold construction begins.
Tolerances and Fit
Tighter tolerances increase tooling precision, inspection demands, and production sensitivity. Each dimension should receive a tolerance based on its function rather than a universal specification. Mating parts require attention to shrinkage, temperature changes, and the resin’s behavior during cooling.
Choosing a Suitable Resin
Resin selection affects strength, flexibility, heat resistance, chemical resistance, appearance, and cost. Common material groups include thermoplastics such as polypropylene, ABS, nylon, polycarbonate, and polyethylene. Each resin has different flow characteristics and shrinkage behavior.
A part exposed to heat needs a resin rated for its operating temperature. A part that faces impact requires suitable toughness, while a part that touches chemicals needs documented resistance to those substances. Additives, glass fibers, colorants, and recycled content also affect processing and final performance.
Material data should match the intended application and molding equipment. The resin supplier’s processing guidance provides starting values for drying, barrel temperature, mold temperature, and injection speed.
Building and Testing the Mold
A mold usually contains a cavity, a core, cooling channels, an injection system, and an ejection system. Steel and aluminum provide different balances of durability, machining time, and expected production volume. The chosen material should match the number of parts, surface requirements, and maintenance plan.
The gate controls how resin enters the cavity, while runners carry material through the mold. Proper gate placement reduces weld lines, air traps, and uneven filling. Venting gives displaced air a path out of the cavity and helps prevent burns or incomplete fills.
A mold trial checks filling, cooling, ejection, dimensions, and appearance. Trial parts should be measured against approved drawings, not judged by appearance alone. Design changes are less expensive before production quantities increase.
Managing Production Quality
Operators monitor shot size, injection pressure, holding pressure, cycle time, and mold temperature during production. Stable settings produce consistent parts and make defects easier to trace. Common defects include short shots, flash, sink marks, warpage, burn marks, and flow lines.
Inspection should cover critical dimensions, fit, surface condition, color, and weight when weight indicates filling consistency. A written inspection plan identifies sampling frequency, measurement methods, and acceptance limits. Process records also help separate material problems from tooling or machine problems.
Preventive mold maintenance includes cleaning vents, checking ejector movement, inspecting cooling passages, and protecting steel surfaces. Maintenance intervals should reflect cycle count and mold conditions rather than a fixed calendar date.
Conclusion
Successful injection molding begins with a part that suits the process, a resin that meets its service demands, and a mold that supports controlled filling and cooling. Designers should review wall thickness, draft, tolerances, gates, vents, and ejection before approving tooling. The next practical step is to create a part review checklist, then confirm material data, critical dimensions, and inspection methods with the molding team before the mold enters production.

Comments